Thermoforming Scrap Grinder — Inline Sheet Skeleton Recycling
When cups and trays are punched from sheet, 30–50% of that sheet leaves the press as skeletal web. A thermoforming scrap grinder turns the skeleton back into regrind for your sheet extruder — RE-series models from 35 to 1,200 kg/hr.
The Thermoforming Scrap Challenge
Thermoforming is geometrically wasteful by design. Cups, glasses, trays and clamshells are round or rounded; the sheet they are punched from is rectangular. Whatever the layout of the forming tool, the skeletal web left after punching typically carries 30–50% of the sheet away as scrap — on every roll, all shift long. Add edge trims from the sheet line, start-up sheet run before gauge stabilises, and formed rejects, and a cup or tray plant generates scrap at nearly the same rate as product.
The skeleton itself is awkward material: a continuous lattice of thin film that tangles, traps air and occupies enormous volume per kilogram. Left unground, it fills the plant — and PS, PP and PET sheet plants in India cannot afford that, because the skeleton is premium material. Most Indian thermoformers extrude their own sheet, which means every kilogram of skeleton reground and returned to the sheet extruder directly displaces a kilogram of virgin granule. A plant that punches 40% of its sheet into the scrap stream and does not regrind it is effectively buying 40% more resin than it sells.
Grind the Skeleton Inline, Feed the Extruder Back
The standard solution is a grinder stationed at the end of the forming line. Skeleton web and trims go into the hopper as they come off the press — fed steadily, or cut into manageable lengths if your line winds the skeleton onto rolls. Inside the chamber, the 5-blade rotor cuts the thin sheet against a mesh screen sized to your regrind spec, producing free-flowing flake that stores densely and doses cleanly. Because the scrap is your own sheet — known polymer, known formulation, ground minutes after forming — it is the cleanest regrind a plant can make.
Sizing follows line throughput. A single forming line is usually well served by an RE12 (60–80 kg/hr) or RE16 (150–250 kg/hr) grinding inline; plants running several lines, or grinding centrally at the sheet plant, step up to the RE20–RE40 models at 250–1,200 kg/hr. One material note: PS and PP regrind can return to the sheet extruder after simple dry storage, but PET is hygroscopic — PET flake must be properly dried before re-extrusion or it loses melt strength. Keep colours segregated, keep the regrind covered, and the loop runs indefinitely.
The Sheet-to-Sheet Recycling Loop
- Collect the skeleton Skeletal web comes off the trim press continuously — wound on rolls or guided straight to the grinder
- Keep streams separate PS, PP and PET webs and colours are never mixed — one polymer per grinding run
- Grind to flake The rotor cuts web, trims and rejects against the mesh screen into uniform, dense regrind flake
- Store dry — and dry PET Flake is stored covered and moisture-free; PET regrind is dried before it goes anywhere near the extruder
- Re-extrude into sheet Regrind blends with virgin granule at the sheet extruder — back into the same rolls it came from
Recommended Machines for Thermoforming Scrap
All from the RE-series plastic grinder line — pick the model that matches one forming line or your whole plant.
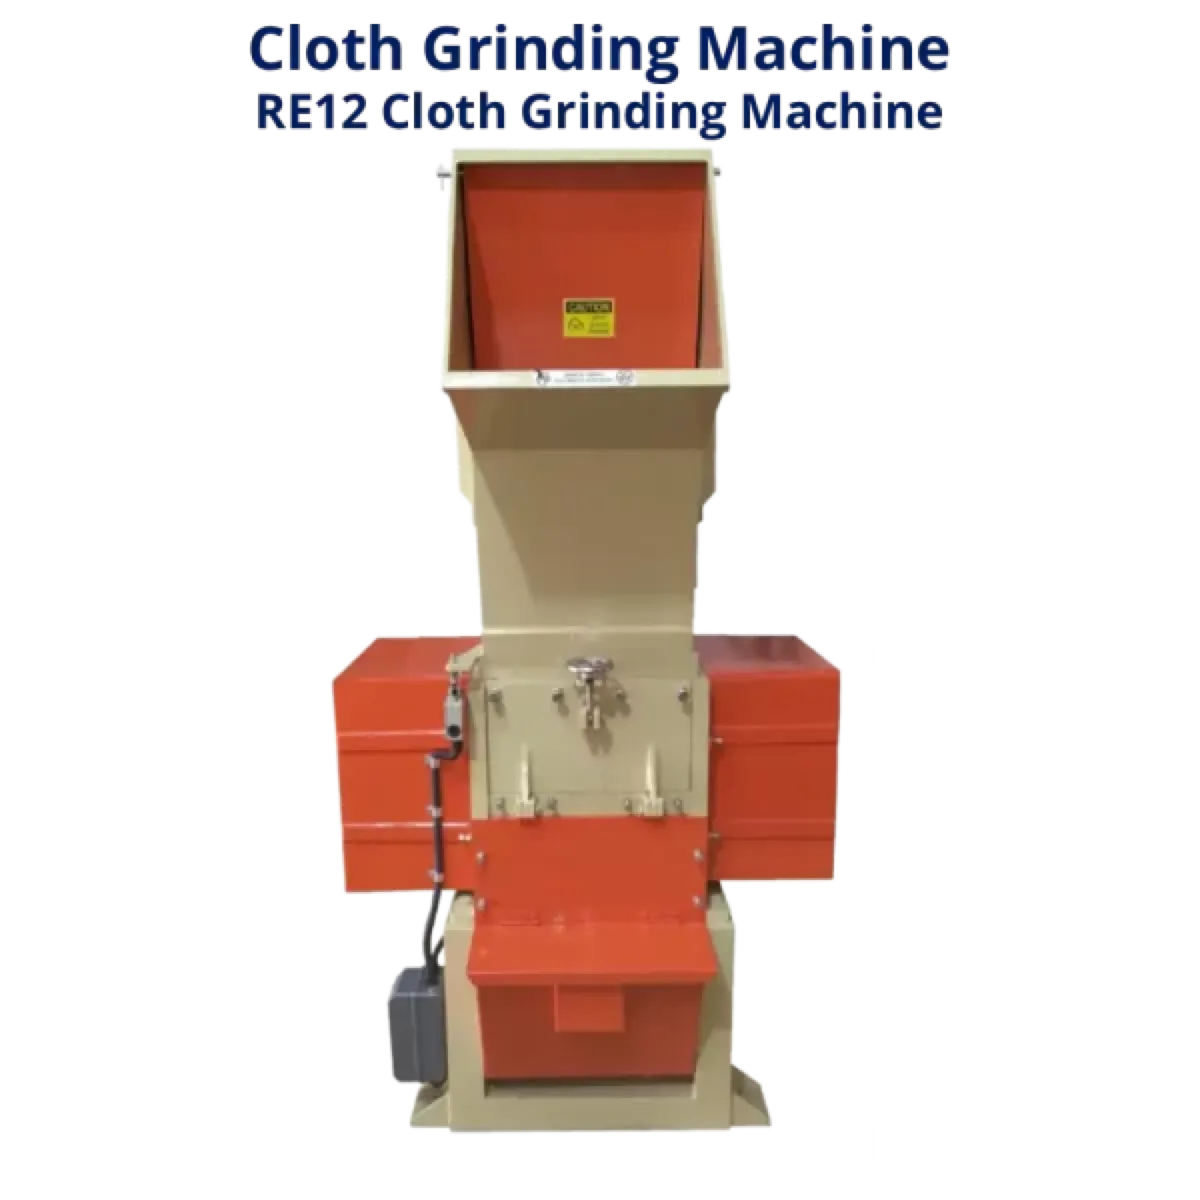
Plastic Grinder — RE12 (Inline)
Single-line duty · compact footprint
- Capacity: 60–80 kg/hr
- Power: 5 HP
- Throat: 12″ × 12″
- Footprint: 1100 × 950 mm · 450 kg
Best for: one forming line grinding its own skeleton and trims at the end of the press.
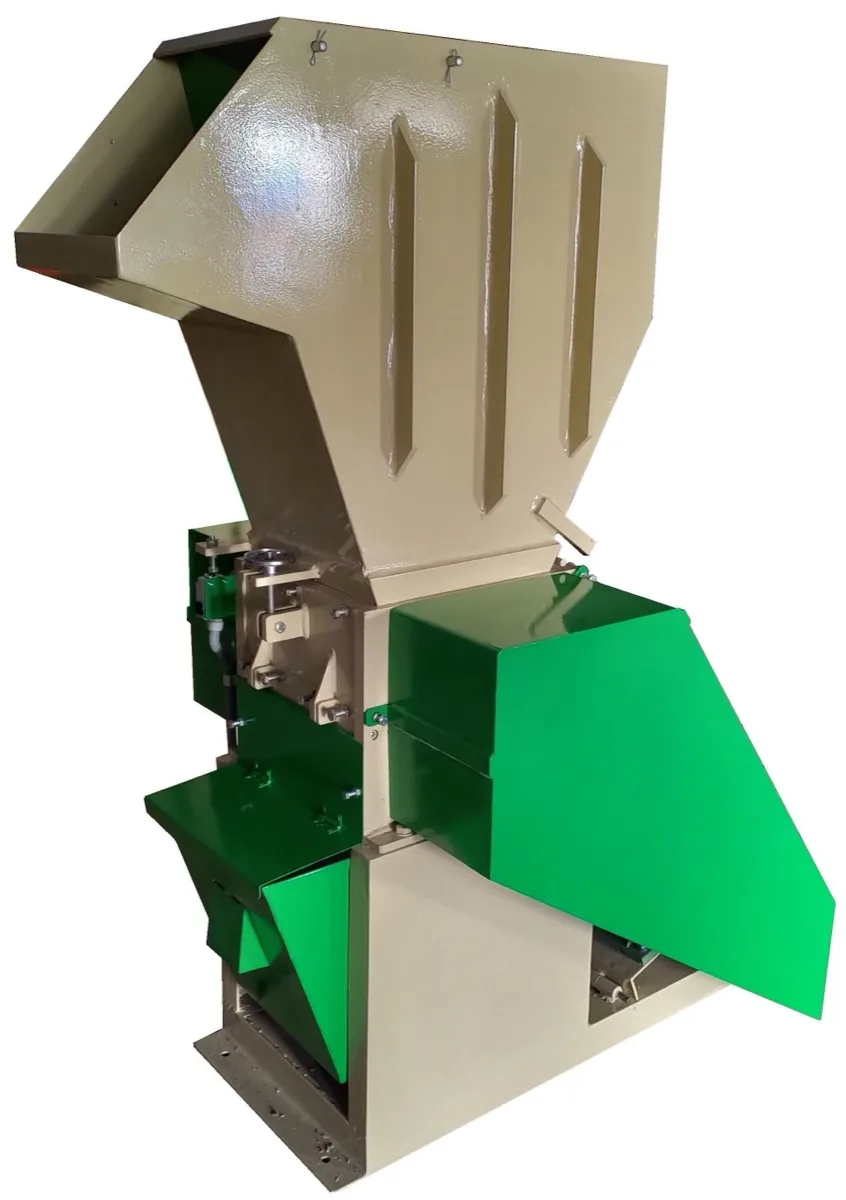
Plastic Grinder — RE16
High-output line duty · 16″ throat
- Capacity: 150–250 kg/hr
- Power: 10 HP
- Throat: 16″ × 16″
- Takes stacked formed rejects whole
Best for: fast cup and glass lines where skeleton plus rejects exceed the RE12’s range.
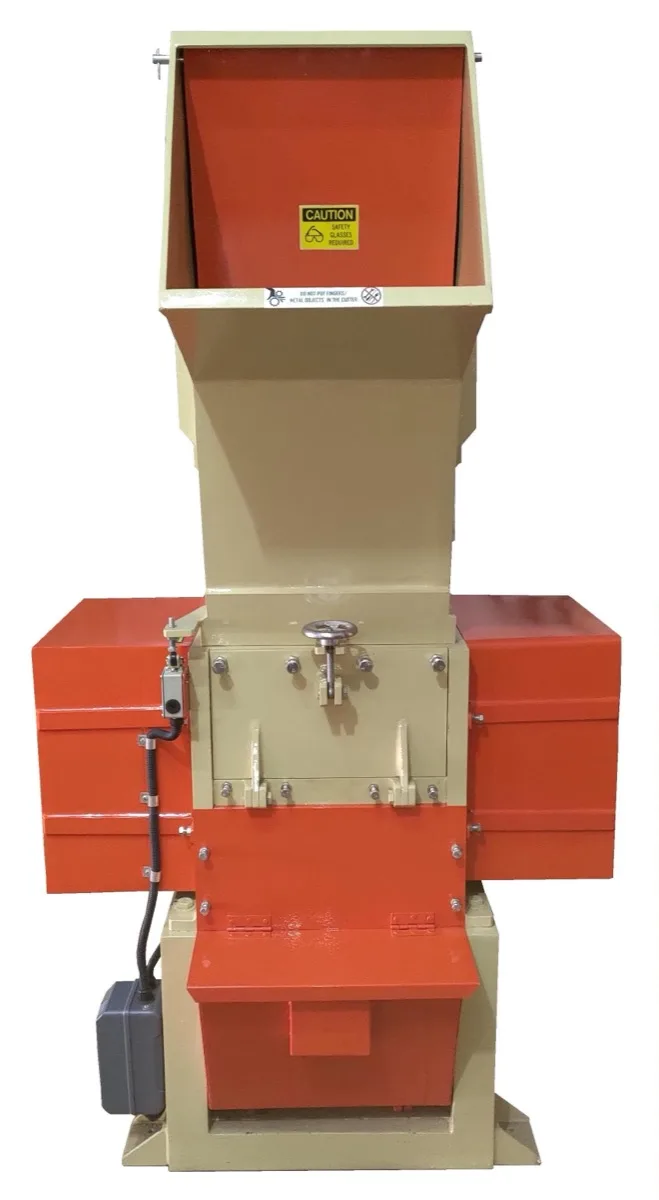
Plastic Grinder — RE20–RE30 (Central)
Multi-line plants · batch grinding
- Capacity: 250–800 kg/hr
- Power: 15–30 HP
- Throat: 20″ × 20″ to 30″ × 30″
- 5 blades per set; overload-protection starter
Best for: sheet plants grinding skeleton rolls from several forming lines at one central station.
Technical Specifications Comparison
| Specification | RE12 | RE16 | RE20 | RE30 |
|---|---|---|---|---|
| Motor power | 5 HP | 10 HP | 15 HP | 30 HP |
| Grinding capacity (15 mm screen) | 60–80 kg/hr | 150–250 kg/hr | 250–400 kg/hr | 600–800 kg/hr |
| Throat size | 12″ × 12″ | 16″ × 16″ | 20″ × 20″ | 30″ × 30″ |
| Blades (rotating + fixed) | 3 + 2 | 3 + 2 | 3 + 2 | 6 + 4 |
| Machine weight (approx.) | 360 kg | 950 kg | 1,062 kg | 3,000 kg |
| Best for | One forming line | Fast line + rejects | 2–3 lines, central | Multi-line sheet plant |
| Get Quote → | Get Quote → | Get Quote → | Get Quote → |
Not sure which grinder fits your forming lines?
Tell our technical team your sheet material, line speed and skeleton percentage — we’ll recommend the right model, free.
Why Choose Raj Electricals
Disposables and packaging converters across India run our grinders — built in Mumbai since 1985, serviced pan-India.
Frequently Asked Questions
How much of a thermoforming sheet actually becomes scrap?
More than in almost any other plastics process. The skeletal web left after parts are punched typically carries 30–50% of the sheet area away as scrap — round cups punched from rectangular sheet sit at the high end, tight-nested trays at the low end. Add sheet-line edge trims, start-up sheet and formed rejects and total scrap often approaches half the resin consumed. That is precisely why nearly every serious thermoforming plant grinds its skeleton and runs sheet with a regrind blend.
Can skeleton regrind really go back into food-grade cups and trays?
The skeleton is your own sheet, ground minutes after forming — it never left the plant or touched food, which is why sheet-to-sheet recycling of in-house skeleton is standard practice across the industry. Quality holds when the basics hold: one polymer and colour per stream, regrind stored covered and dry, and a consistent blend ratio at the extruder. For specific food-contact compliance on your product, confirm against the applicable FSSAI/IS norms for your sheet construction — multilayer and coated sheets need more care than mono-material PS or PP.
Does PET sheet scrap need different handling from PS and PP?
Yes, in one important way: moisture. PET is hygroscopic, and wet PET flake degrades sharply in the extruder — losing intrinsic viscosity and melt strength, which shows up as brittle sheet. PET regrind must be dried before re-extrusion, so plan drying capacity alongside the grinder. PS and PP are far more forgiving and need only clean, covered storage. The grinding step itself is identical for all three — the RE-series grinder handles PS, PP and PET sheet without changeover beyond a clean-down between materials.
Will thin skeleton web tangle or bridge in the grinder?
Thin web needs steady feeding, not dumping. Fed continuously off the line — or in cut lengths if you wind skeleton onto rolls — the web draws into the rotor and cuts cleanly against the screen. Problems start when a whole compressed bundle is forced in at once. The overload-protection starter trips the motor on a jam rather than letting it damage anything, but disciplined feeding means it rarely has to. During a trial we will show you the feeding rhythm on your own web.
What size grinder do I need for my forming line?
Calculate your scrap rate: sheet consumption per hour multiplied by your skeleton percentage. A line consuming 150 kg/hr of sheet at 40% skeleton generates 60 kg/hr of web — an RE12 at 80 kg/hr covers it with headroom; faster lines or lines with heavy reject loads step up to the RE16. Central grinding across multiple lines points to RE20–RE30. Our machine selection guide walks through the arithmetic, or send your line details for a free recommendation.
How much does a thermoforming scrap grinder cost in India?
Every machine is quoted to the job. What moves the number is capacity, throat size, motor rating, MS or SS construction and the automation you add — a blower, a conveyor, a control panel. Our guide to what drives machine cost walks through each of those; send us your material and daily volume and we will size the machine and quote it, usually the same day.
Can I trial the grinder on my own sheet skeleton before buying?
Yes — bring rolls or bags of your actual skeleton, trims and rejects to our works at Andheri East, Mumbai, and we will grind them so you can verify flake size, throughput and feeding behaviour on your exact material and gauge. Outstation plants can request a video trial. Contact us to book a slot — Mon–Sat, 9 AM to 7 PM.
Get a Free Quote for a Thermoforming Scrap Grinder
Tell us your sheet material, line throughput and skeleton percentage — our technical team responds with a model recommendation and firm pricing, usually within one working day. No spam, no obligation.
102/103/104, Madhu Industrial Estate, Old Nagardas Road, Mogra Lane, Andheri East, Mumbai – 400069
Mon–Sat, 9:00 AM – 7:00 PM
Related Solutions
Extrusion Scrap & Purge Shredding
Your sheet line’s purge lumps and start-up waste need shredding before grinding — the two-stage system.
Learn more →
Injection Molding Scrap Grinding
Sprues, runners and rejects reground beside the press — the same closed-loop logic, different process.
Learn more →
PP (Polypropylene) Waste Shredding
PP sheet, cups and containers from the material side — shredding and grinding across all PP scrap forms.
Learn more →